20.10.2026
Companies
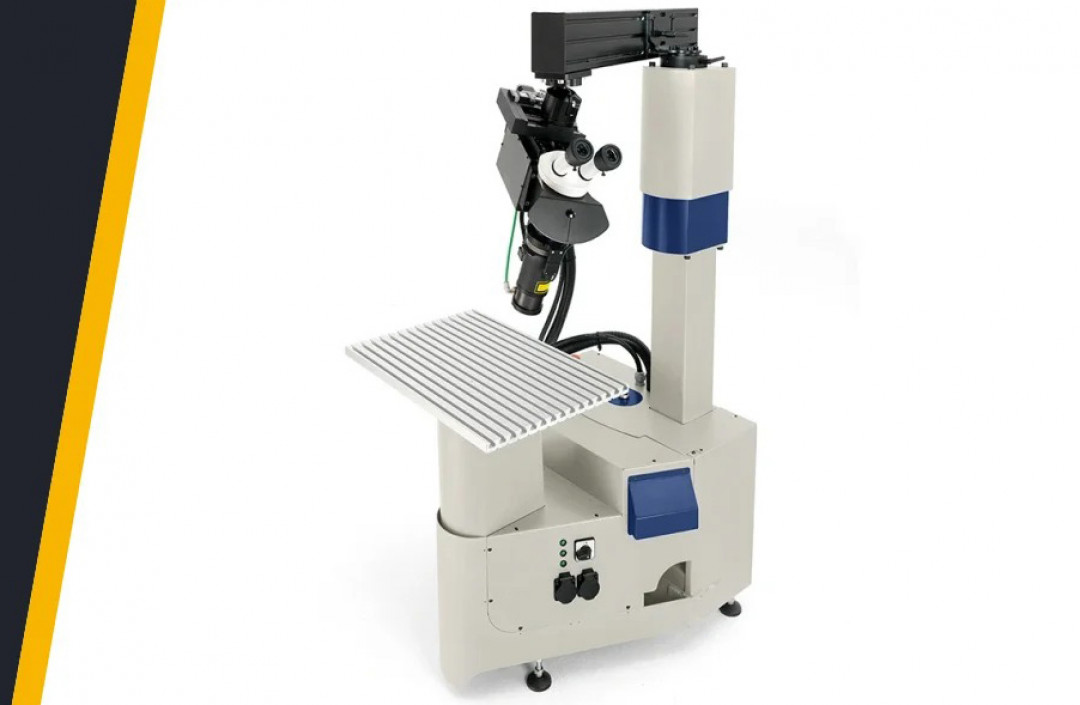
Pulsed mode with pulses from 0.05 ms keeps heat input low, CW suits long seams, SPT protects crack-sensitive alloys: the mode is set before the parameters. Operators often open the parameter screen first. Choosing the operating mode comes earlier and is simpler. The step-by-step guide to switching between CW, pulsed and SPT modes shows the steps on the control. This piece is a three-question decision aid.
Question one: what does the material tolerate?
SPT modulates the pulse on a microsecond scale and keeps the heat-affected zone small on sensitive or reactive grades. For general work, pulsed delivers controlled bursts with minimal distortion.
- High-carbon tool steels: SPT keeps heat input local.
- Titanium and other reactive alloys: SPT should be used for fine control.
- Stainless steels for general maintenance: pulsed mode.
- Mixed or unknown special alloys: starting with pulsed, verifying with a test weld.
Question two: what does the joint need?
Fine spot repairs, edge build-ups and localised seams point to pulsed for precise heat input and low distortion. Long, uniform seams and thicker sections suit CW on the Fibre series, but manage heat input on heat-sensitive parts. On Sigma Laser systems, the series sets the options: the Light series uses a pulsed Nd:YAG source at 1064 nm and supports pulsed mode and SPT, not CW. The Fibre series uses a ytterbium fibre source at 1070 nm and supports pulsed, CW and SPT. SPT is available on all six Sigma Laser systems. Selecting CW on a Light series system is not possible; the hardware does not support it. In practice a Light series system covers repair and fine work, while the Fibre series adds seam welding in series production.
Question three: what is the test weld telling?
The mode is selected on the contol, then parameters and results confirmed with a test weld before production. Whether the seam form and heat tint meet the requirement can be checked at this point and the window can be refinded. "We decide the mode by the material and the joint, never by habit. For titanium and high-carbon tool steels that usually means SPT, and a test weld then shows within minutes whether the window is right," says Alexander Bellouzi, Senior Design & Engineering at Sigma Laser. Where material, joint and parameters do not fall into place on the first attempt, a second opinion saves test time.
(Source: Sigma Laser GmbH)
Schlagworte
FusionHeat InputJoiningLaser Beam WeldingPulsed ModeStainless SteelSteelTitaniumWeld SeamWeldingWelding Parameters