14.11.2026
Unternehmen
Of the ten typical defects found on moulds and dies, nearly all are local and can be repaired by laser build-up welding directly on the tool. A die-casting die with heat-checking on the cavity surface arrives in the toolroom late on Friday. The press stands ready, but production cannot resume until the defect is fixed. The toolmaker’s first step is not to assess the look of the damage, but to identify the steel grade and its heat treatment. This decision guides the entire repair process.
Most defects are local and can be welded in place
Damage on injection moulds and die-casting dies is usually confined to specific areas. The main groups are:
- Edges: chipped or worn parting-line edges, worn sealing and shut-off edges, worn radii and corners
- Cracks: heat-checking cracks on die-casting surfaces (surface only), short cracks at edges
- Erosion and pitting: erosion and pitting from the melt, local surface loss
- Seats and dents: damaged ejector or insert seats, dents from handling
Nearly all of these can be repaired by laser build-up welding directly on the tool. Only through-cracks that run across the entire insert require a new part. For all others, material is added where needed and the tool remains in one piece.
Laser beam build-up welding restores surface without affecting hardness or dimensions
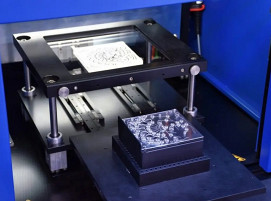
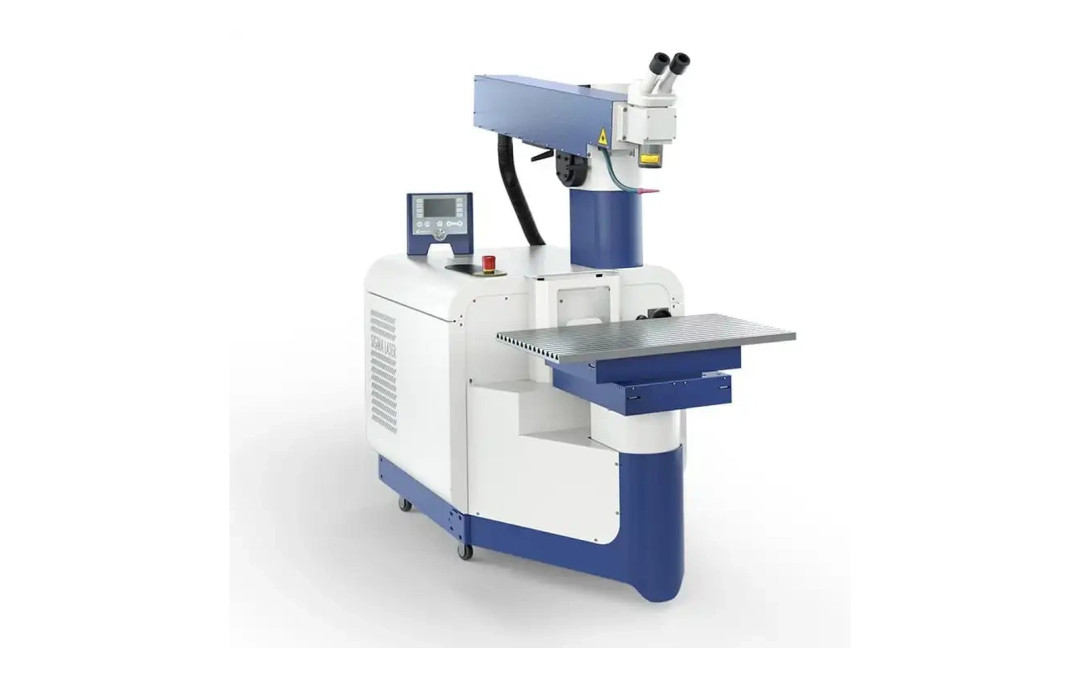
Laser beam build-up welding adds filler wire, matched to the tool steel, at the precise spot indicated by the microscope cross-hair. The process uses pulse energy up to 170 J and peak power up to 13 kW, allowing controlled melting of the filler without significant heating of the surrounding steel. This keeps the tool’s hardness and dimensions intact. Mobile five-axis workstation systems are brought to the mould, whether in the toolroom or next to the press. Swivelling optics reach undercuts and deep cavities, so most repairs do not require dismantling or transport of the tool.
The steel grade as decisive factor of repair
The first step in any repair is to identify the steel grade, such as 1.2344 (H13) or 1.2343, and its heat treatment. Filler wire, pulse shape and any pre-heating are chosen to match the material. High-carbon tool steels are prone to cracking under heat. Super Pulse Technology shapes the pulse to keep the heat-affected zone small, allowing even those steels to be welded without cracks. “In the toolroom people judge a defect by how it looks, but the steel decides the route. I have seen two defects that looked identical and needed completely different settings,” says Alexander Bellouzi, Senior Design & Engineering at Sigma Laser.
(Source: Sigma Laser GmbH)
Schlagworte
AutomationCladdingHeat CracksLaserLaser Beam Build-up WeldingLaser Beam WeldingMouldsSteelWeldingWelding Wire