International
© bielomatik
25.02.2025

Non-Contact Welding Process for Thermoplastic Polymers

In the current issue of our trade technical journal JOINING PLASTICS/FÜGEN VON KUNSTSTOFFEN and in the archive you will find many other interesting articles. Feel free to browse.
Joining Plastics [EN]
Laser-based infrared welding

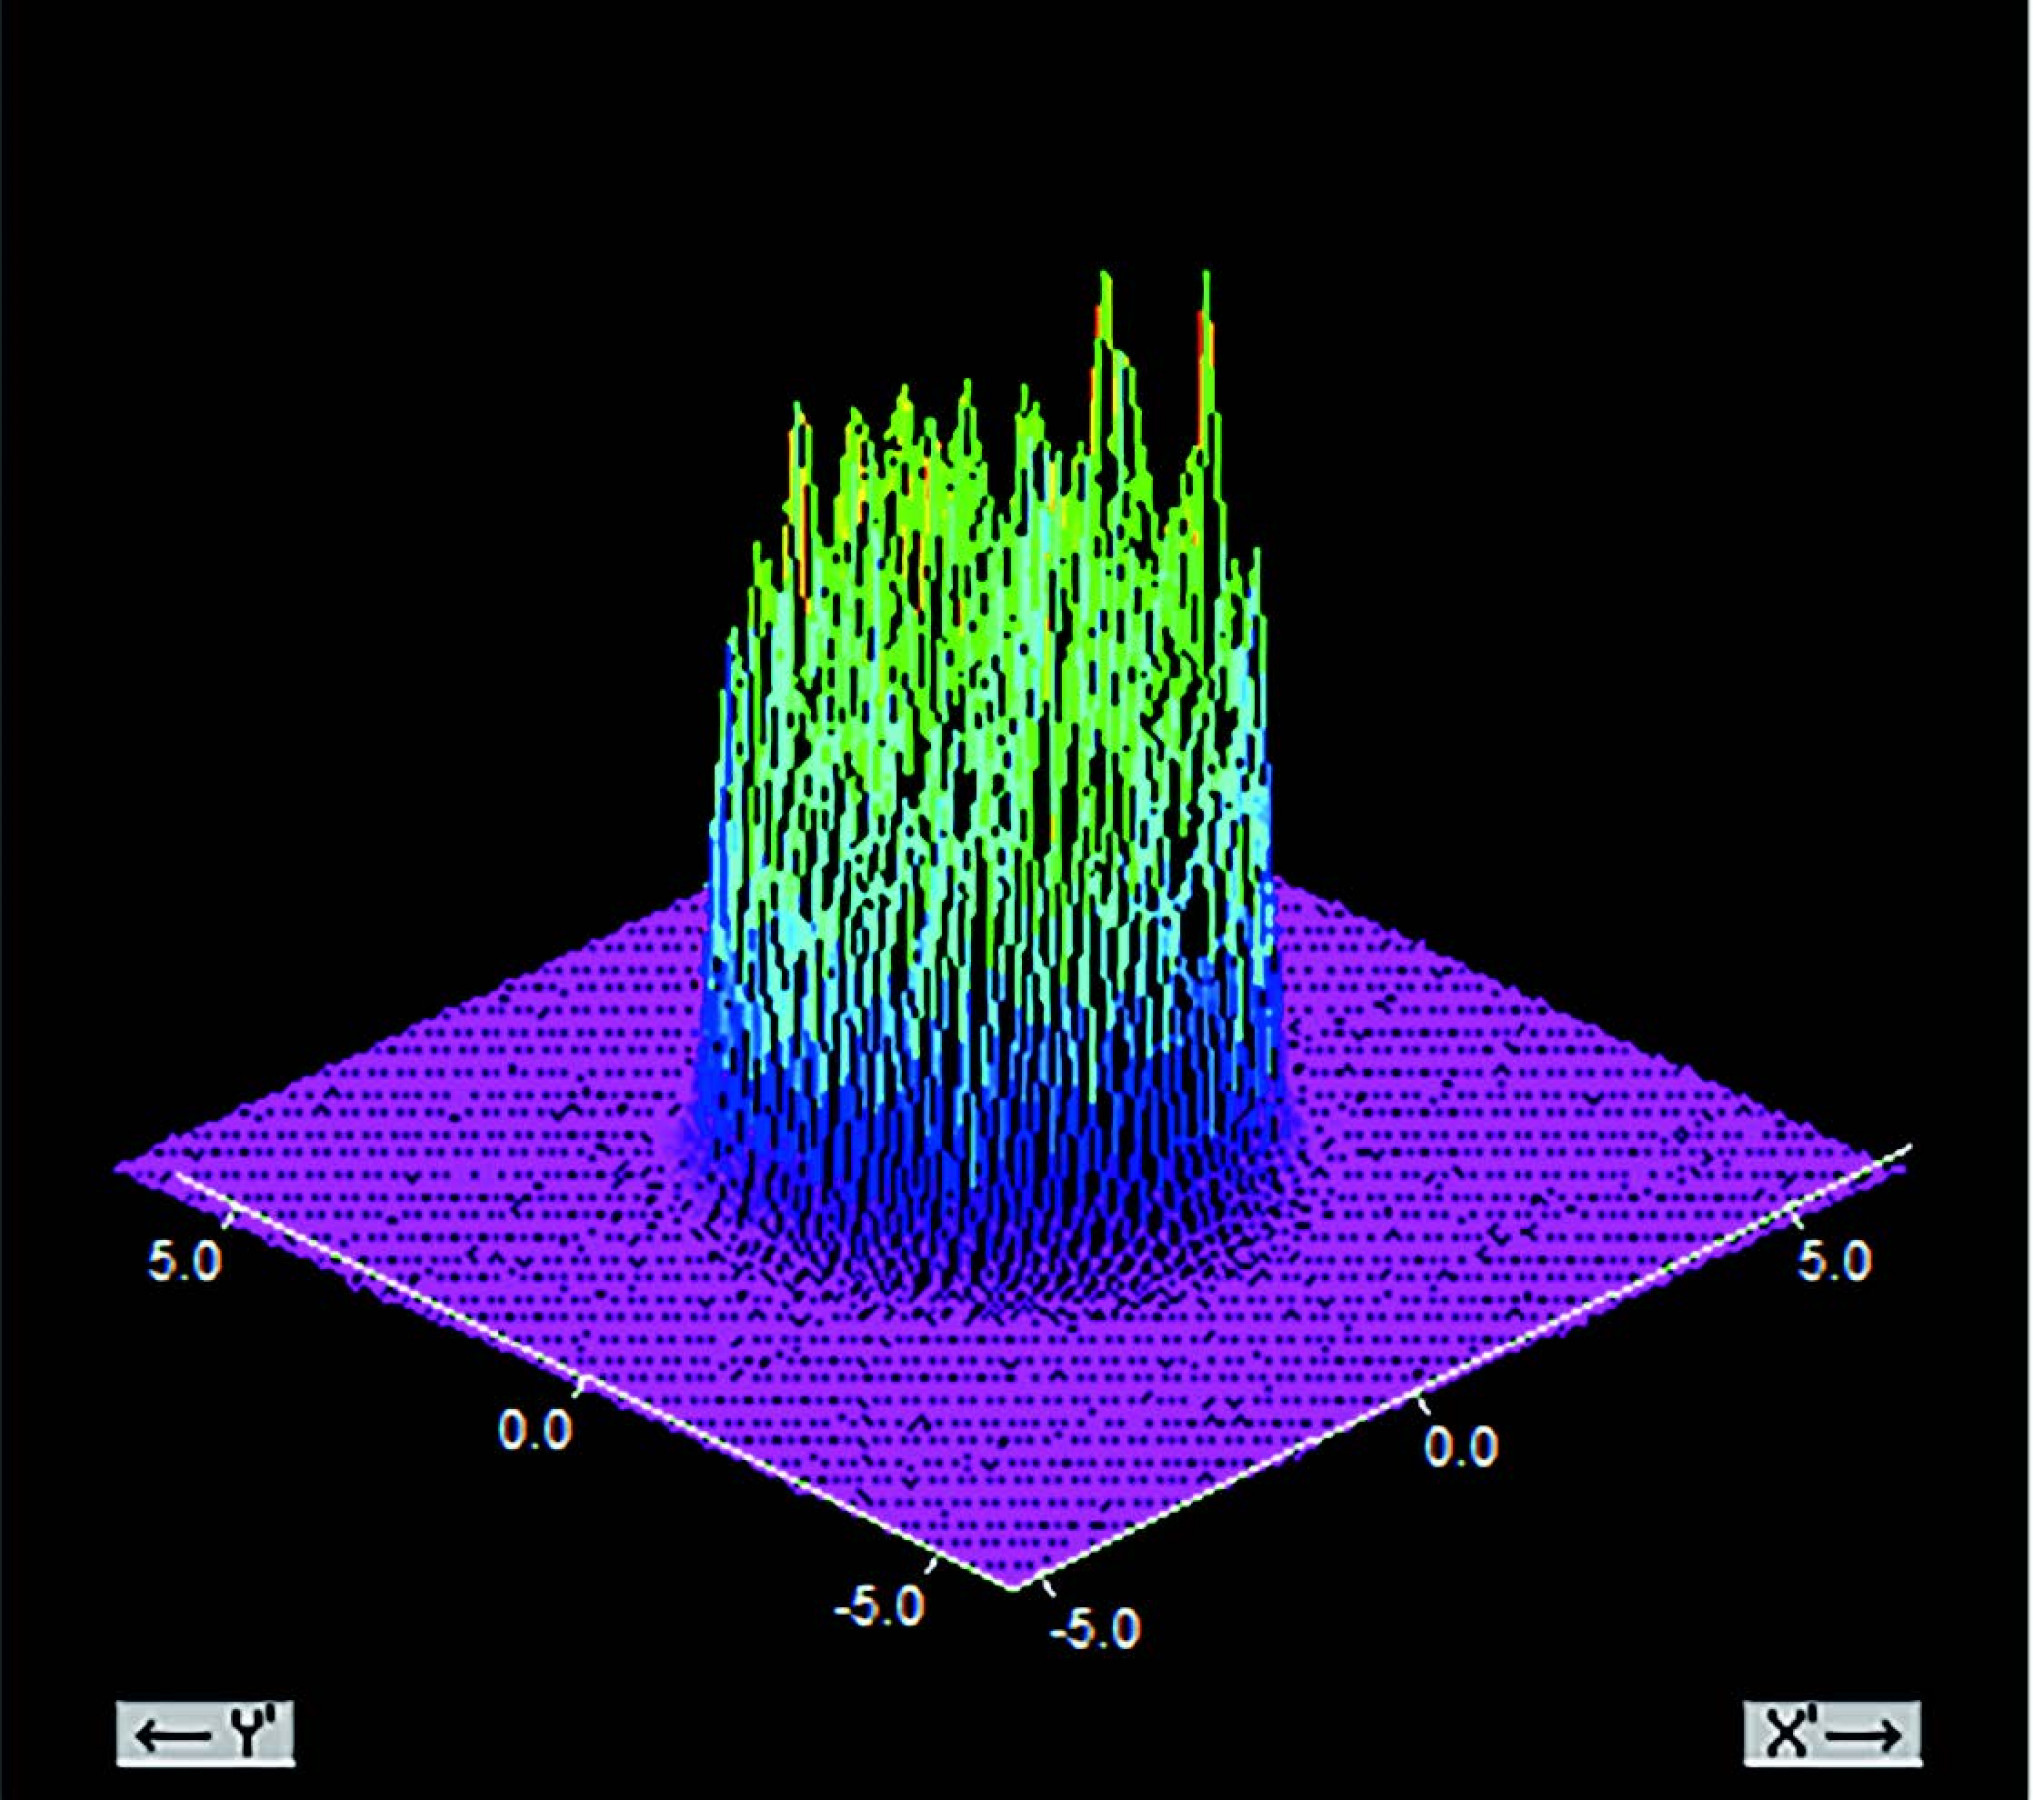
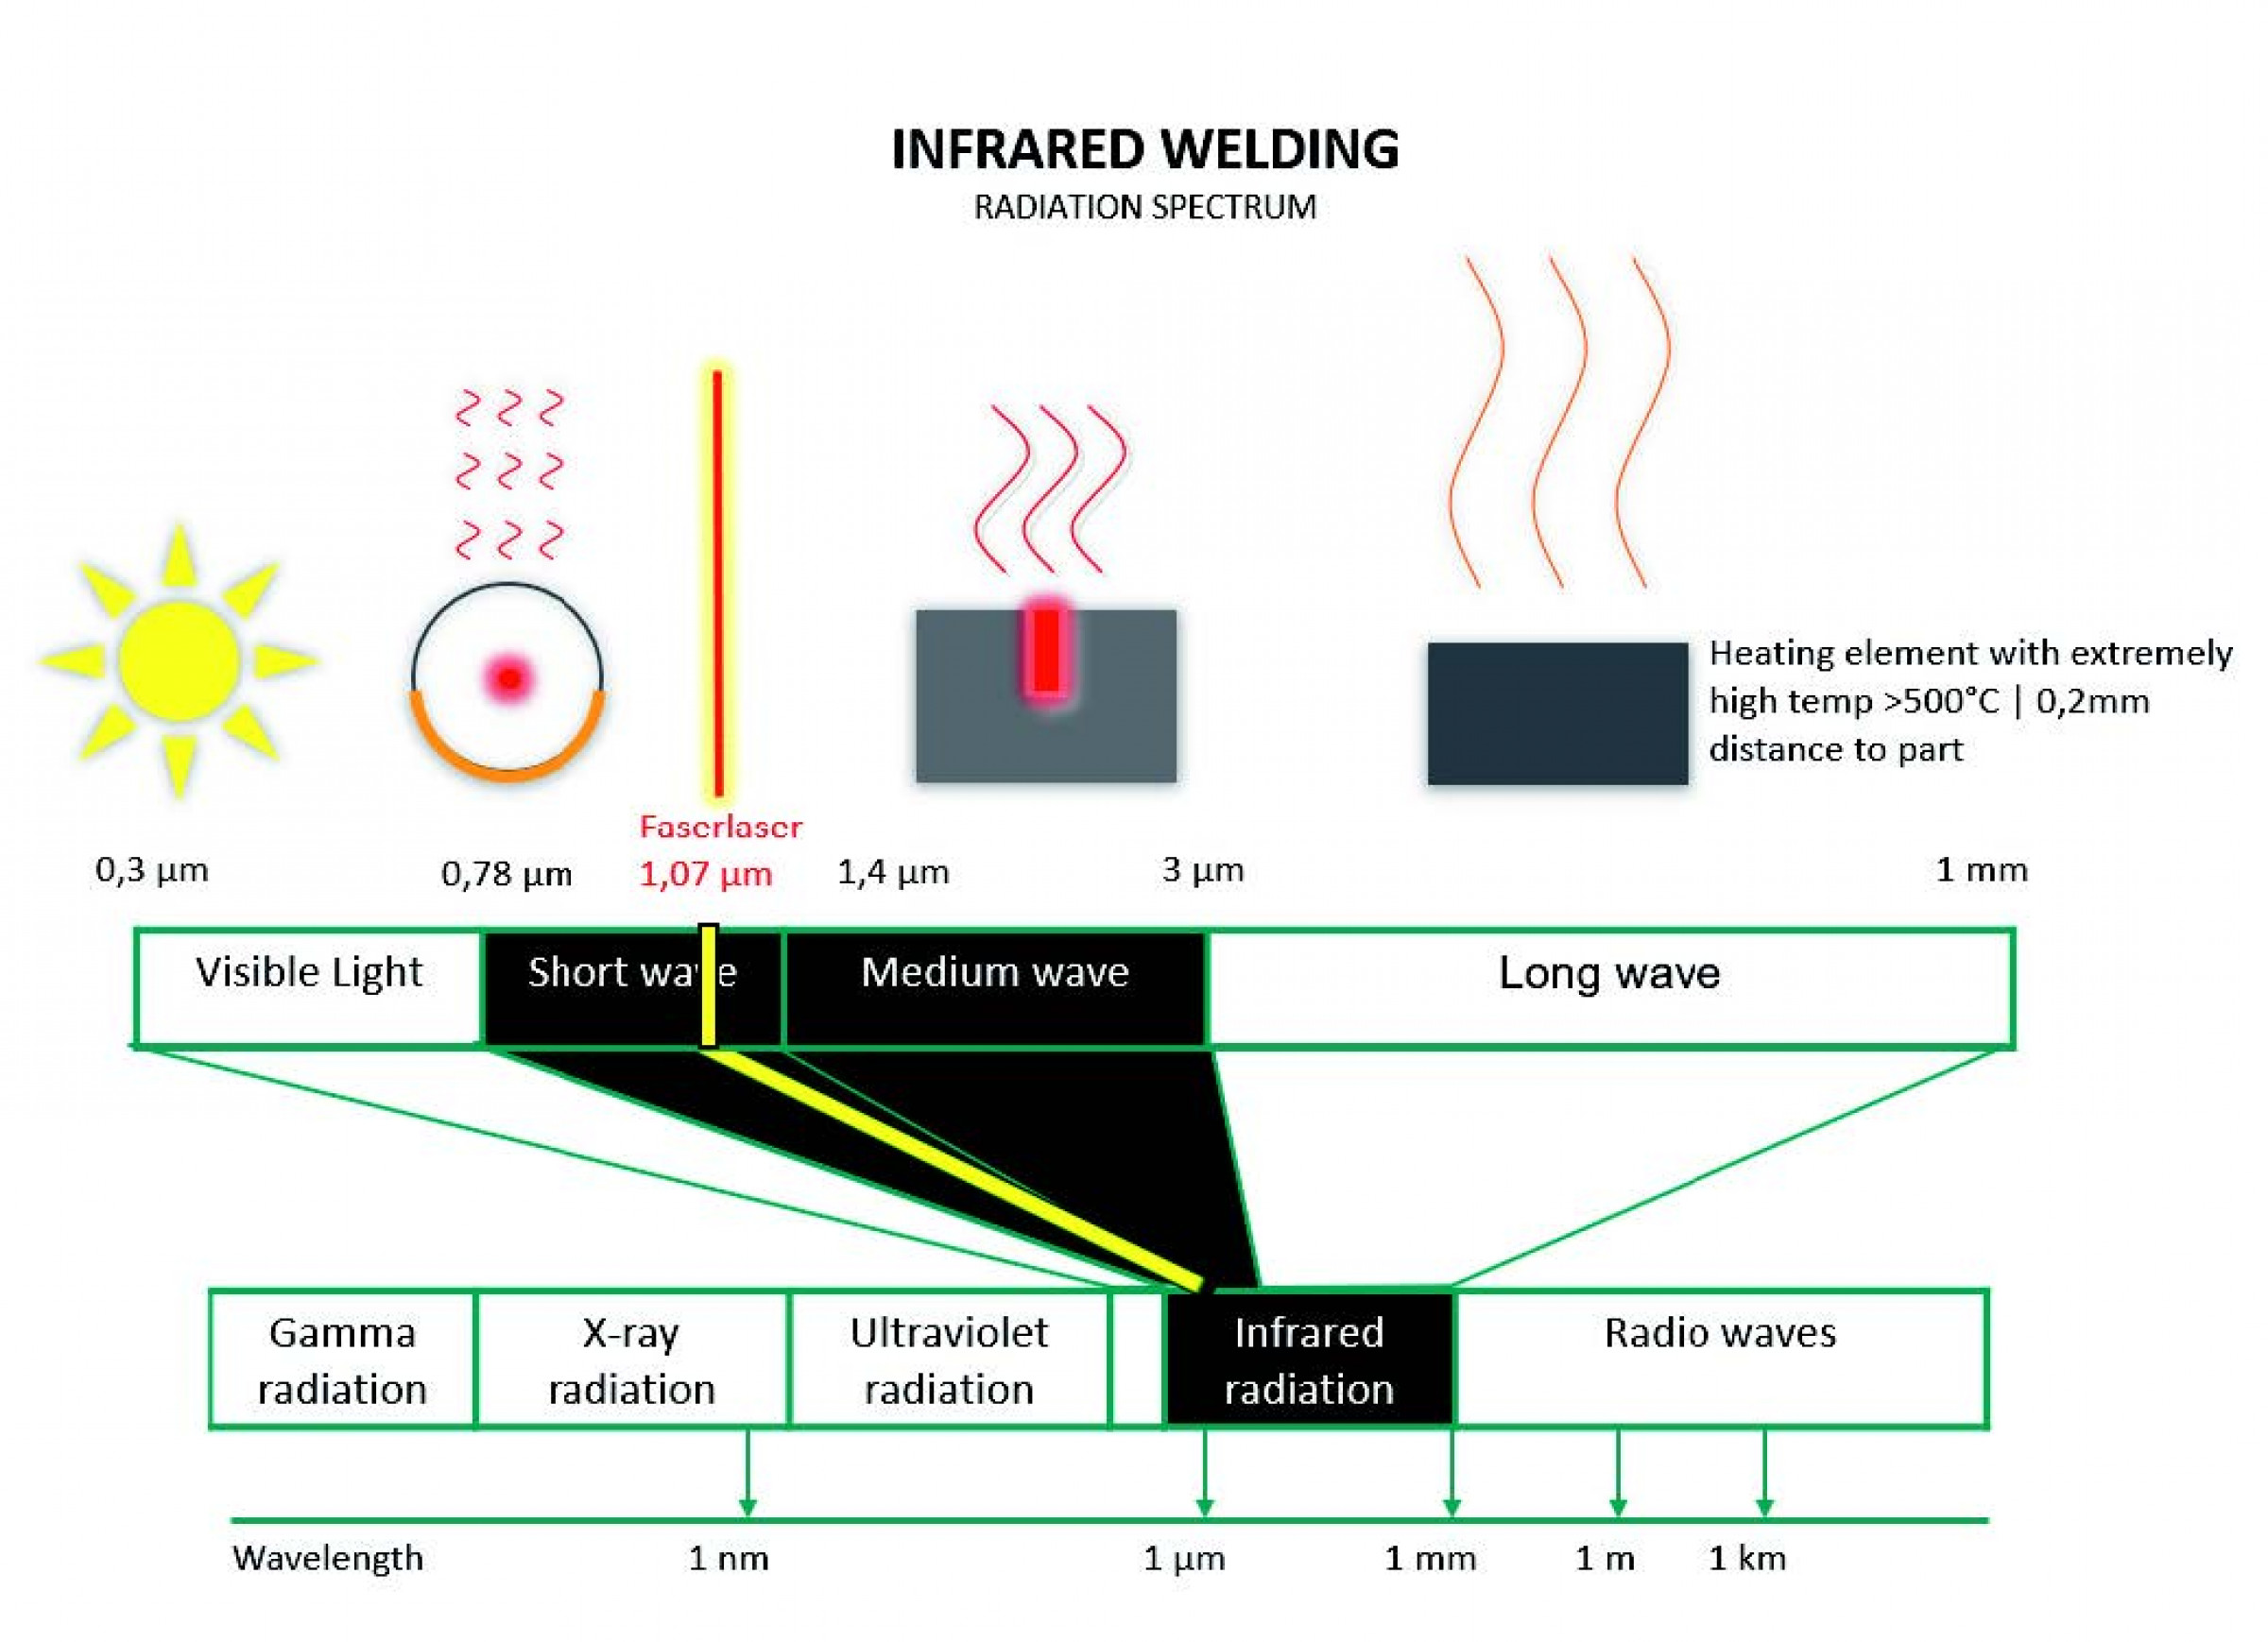
The laser-based infrared welding process further developed by bielomatik differs primarily in the energy source for infrared radiation. Instead of expensive and sensitive infrared tube radiators or metal foil ribbon emitters, a commercially available fiber laser system is used. This system operates in the infrared wave-length range of 1070 nm, Fig. 1. The fiber laser provides a top-hat beam profile, which is ideal for efficiently plasticizing welding ribs. Key technical advantages of laser-based infrared welding:

  1. Maximum flexibility: Using a laser source and a scanner, energy can be transferred almost simultaneously to any geometry.
  2. Reduced investment costs: Tool-investment is reduced by up to 70 %, as the laser-scanner unit serves as a programmable IR emitter that needs to be procured only once.
  3. Increased precision: The laser beam enables highly precise and localized heat input. Complex areas such as T-joints or ring welds can be welded with high accuracy and tight sealing.
  4. More efficient energy transfer: The laser focuses energy directly and specifically on the welding points, reducing energy consumption. This minimizes heat absorption by the components and prevents distortions caused by internal stress release.
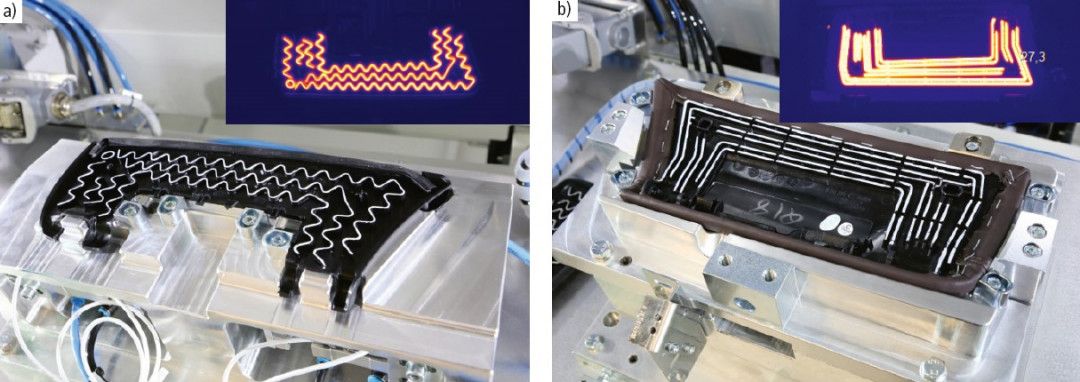
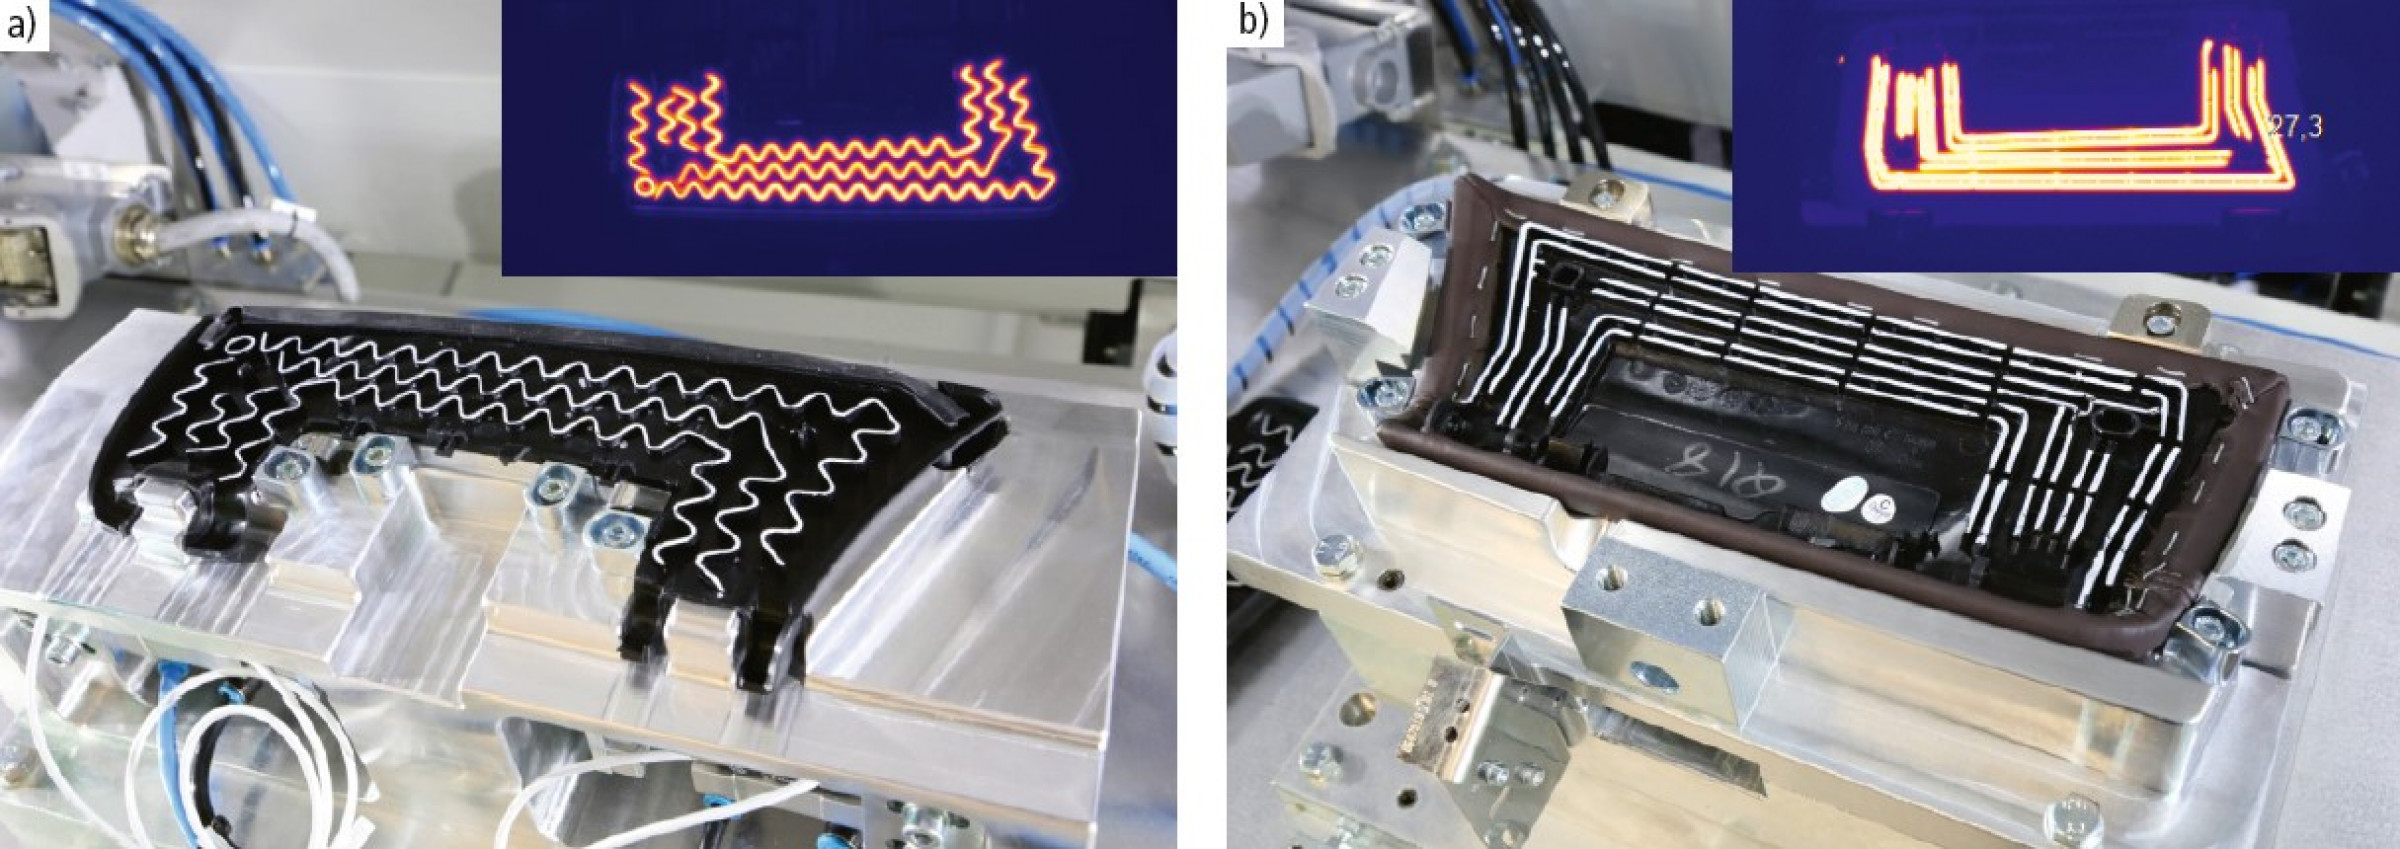
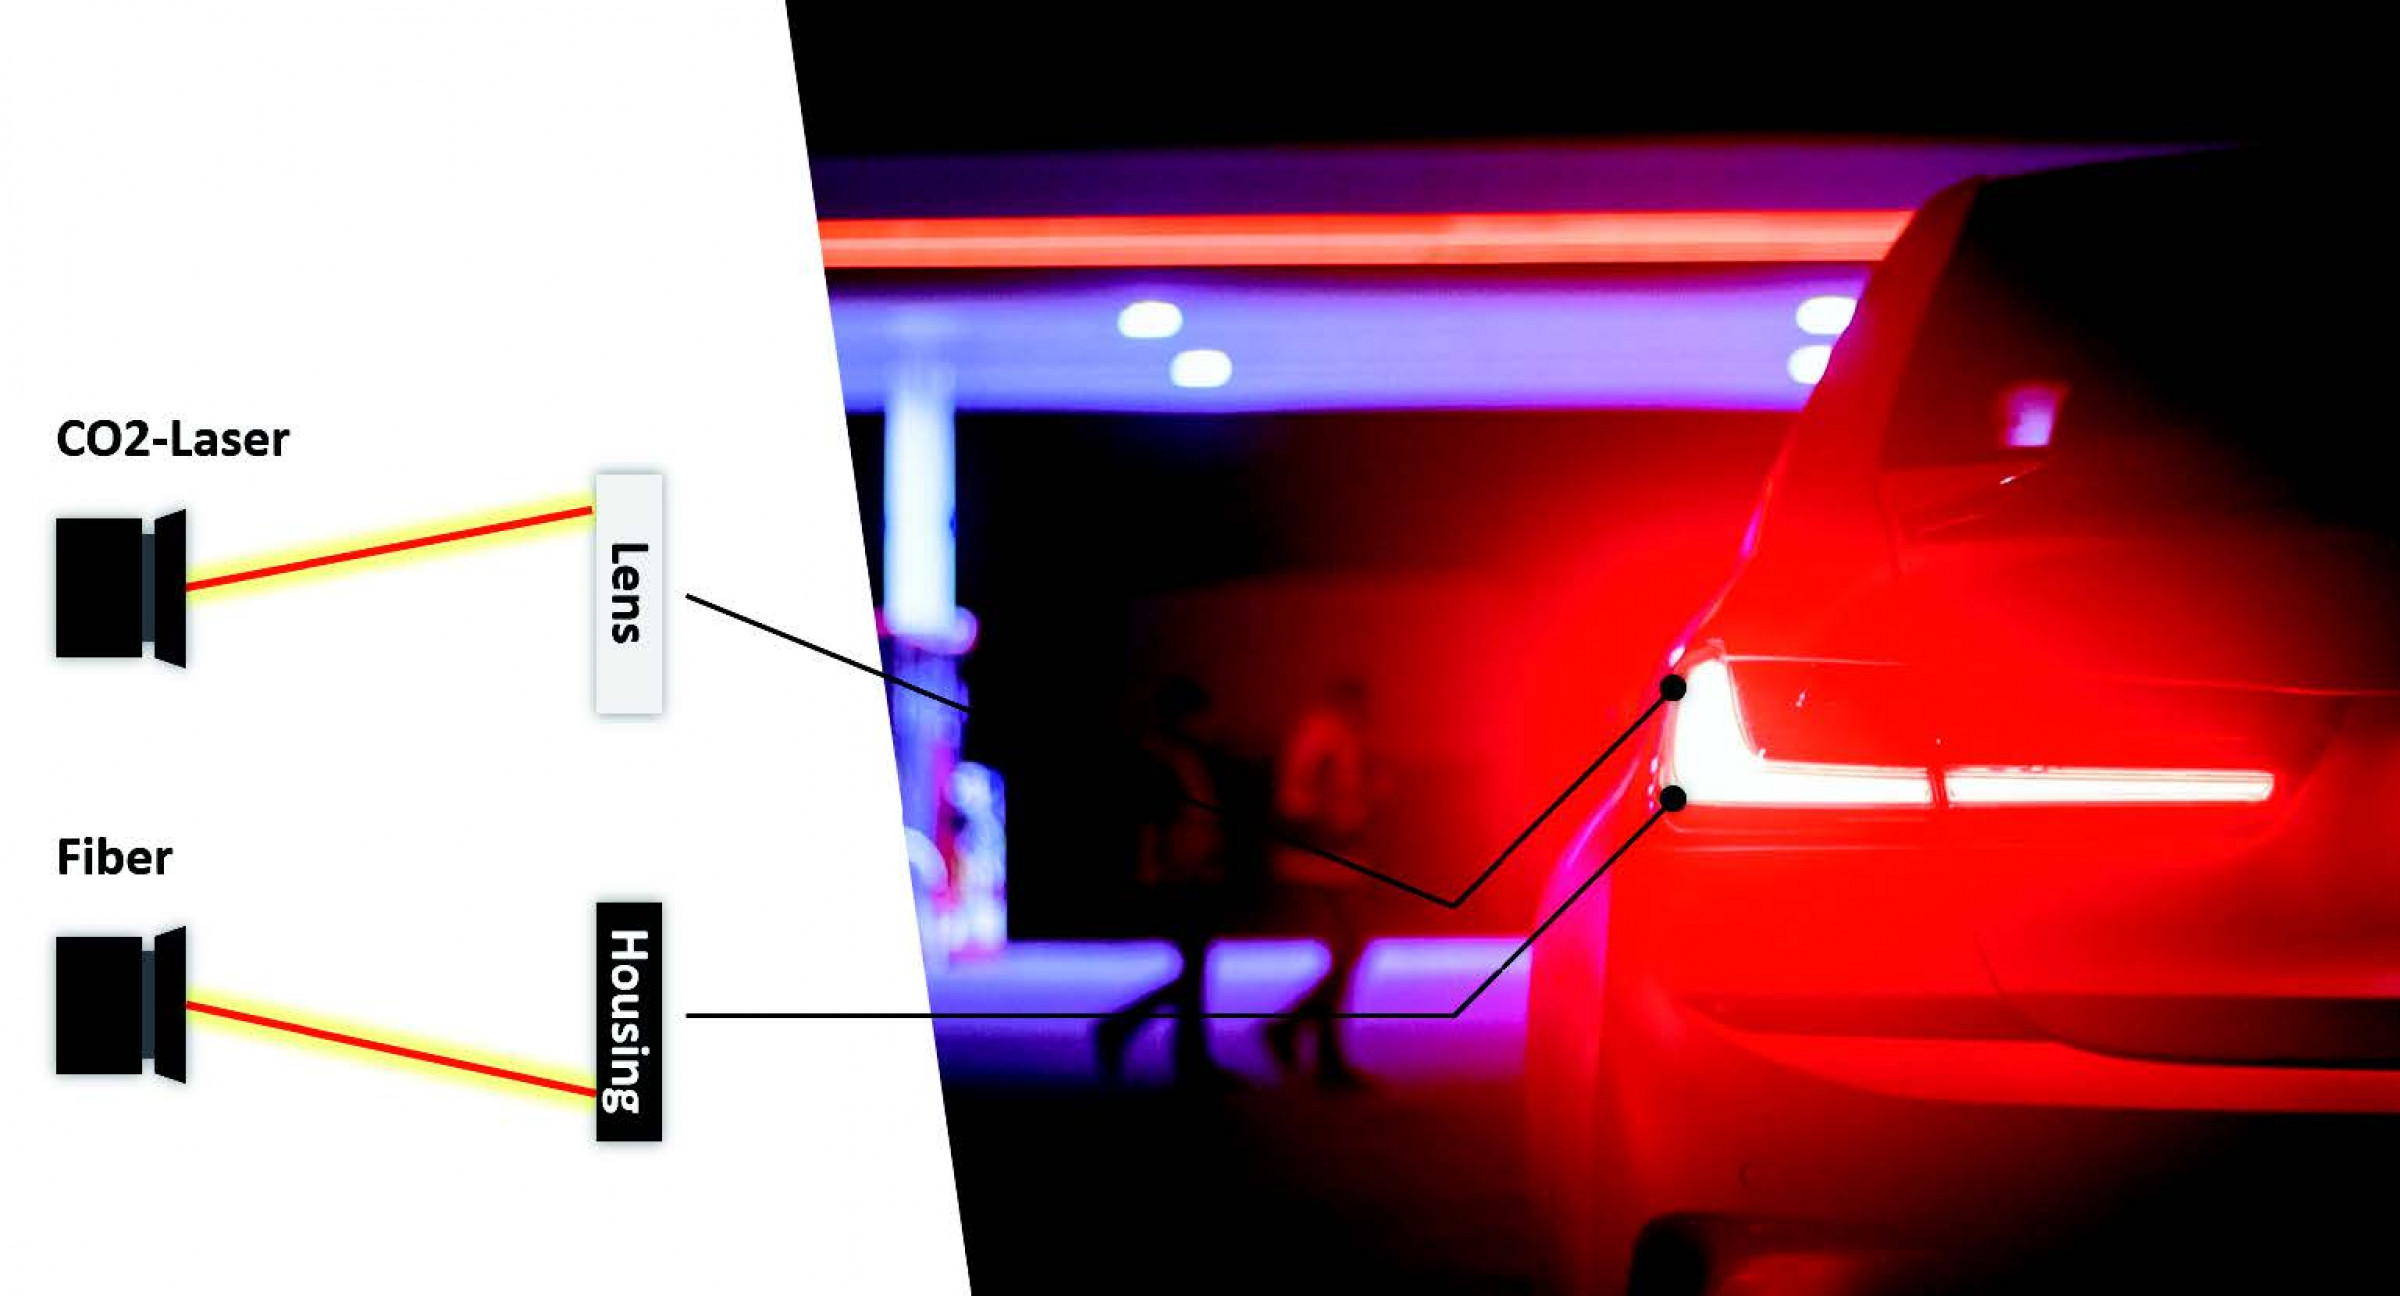
  5. New application opportunities: In a joint development (by bielomatik, LZH and Coherent), a CO2 laser was controlled to allow process-safe, flexible and gentle welding of IR-transparent components. For example, a taillight with a housing made of ABS/PC and a lens made of PMMA (Fig. 4).
Targeted energy transfer

The laser-based infrared welding process offers numerous advantages through its precise energy transfer and high precision:

  • Prevention of thermal material damage: The precise focusing of the laser allows controlled and efficient energy delivery to the weld zone, significantly reducing energy consumption.„
  • Cost-effectiveness and environmental friendliness: The process enables exact control of energy input, tailored to material and geometry, resulting in optimal welding outcomes.
  • Low thermal stress: Heat generation is confined exclusively to the weld zone. The rest of the component remains cool and intact, which is particularly advantageous for temperature-sensitive components.
  • „Shorter commissioning and parameter setting: The programmable IR emitter enables precise, reproducible and transferable parameterization of project data, saving significant time during commissioning and implementation in production processes. This makes it particularly suitable for series production.
Conclusion

The laser-based infrared welding process developed by bielomatik offers significant improvements in precision, efficiency, and material versatility. The process is cost-efficient, sustainable and highly flexible. This technology not only opens new application possibilities, such as in lighting manufacturing, but also provides a very economical alternative to
conventional infrared welding techniques. By combining the advantages of laser scanner systems with the economic and ecological benefits of infrared welding, this process is well-suited for a wide range of production applications, from automo-tive to medical technology. 

(Source: Beatrice Maus, bielomatik)

Schlagworte

EnvironmentInfraredJoining PlasticsLaserPolymerWelding
Verwandte Artikel

18.10.2026

PFAS-freie Antihaft-Beschichtungen für das Kunststoffschweißen

PFAS-frei, verschleißfest und energieeffizient: Mit dem neuen Forschungsprojekt „PTFE-Sub“ entwickeln das Kunststoff-Zentrum SKZ und Innovent innovative Sol-Gel-Beschicht...

Energieeffizienz Fügen von Kunststoffen Heizelementstumpfschweißen Joining Plastics JP Kunststoffschweißen PFAS-frei PTFE Recycling Schweißen
Mehr erfahren
Enclosed orbital welding head (C170, 50.8-168 mm OD). In an enclosed head the joint is surrounded by a gas-filled chamber, which supports OD-side shielding for stainless steel and titanium.
15.10.2026

Orbital TIG Welding of Thin-Wall Stainless Steel and Titanium Tube

What really drives weld-to-weld consistency? This article takes a practical look at the variables that decide consistency and at the questions worth asking before a syste...

ASME BPE AWS D18.2 Enclosed Orbital Weld Head ISO 14732 Orbital GTAW Orbital TIG Welding Shielding Gas Stainless Steel Thin-Wall STainless Steel Tube TIG Titalnium Tube Welding Titanium Tungsten Electrode Grinding Weld Consistency Weld Purge Oxygen Welding
Read more
f.l.t.r.: Timo Clasen, Jürgen Raun, Ronald Pajuelo, Lucas Hammerschmidt, Alexander Graf, Tim von Trebiatowski
15.10.2026

Young Welders Competition "Jugend schweißt" Winners Compete at Arc Cup in China

The winners of the 15th DVS national competition "Jugend schweißt" (Young Welders Competition) 2025 are currently in China to take part in the international Arc Cup.

Competition DVS DVS e. V. DVS Group Gas Metal Arc Welding Gas Tungsten Arc Welding German Welding Society Oxy-Fuel Welding Shielded Metal Arc Welding Skilled Crafts Welding Young Welders Young Welders Competition
Read more
Ivano Poletti (Executive Vice President Sales EMEA) verabschiedet sich Ende 2026 in den Ruhestand.
15.10.2026

Wechsel an der Vertriebsspitze von Rehau

Bei Rehau Water Technologies kommt es zu personellen Veränderungen im Vertrieb. Andreas Zinßmeister tritt als Executive Vice President Sales EMEA die Nachfolge von Ivano...

Fügen von Kunststoffen Joining Plastics JP Management Vertrieb
Mehr erfahren