25.03.2026
International
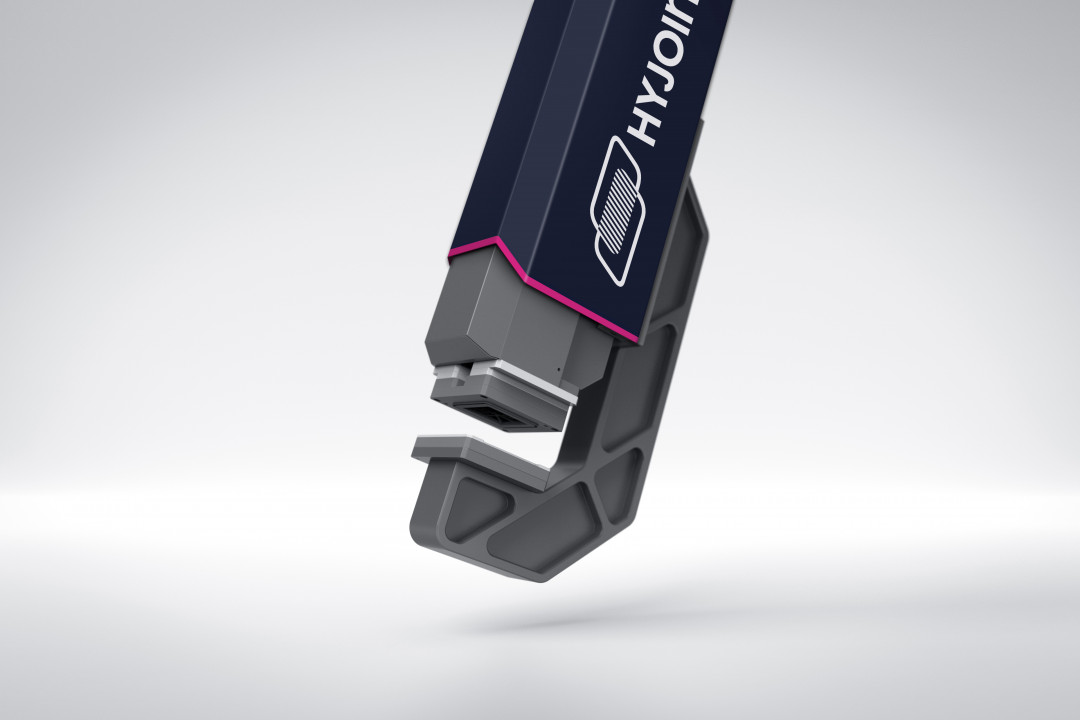
Metal-polymer hybrid components are established in countless applications in our everyday lives. However, in industrial implementation typical challenges remain: demanding pre-treatments, manual processes, difficult automation and high quality assurance and validation costs. At the same time, lightweight construction, sustainability requirements and the circular economy are increasing the need to address joining technologies as a design and strategic topic at an early stage. In the interview, Jakob Wäschenbach, Managing Director of hyjoin GmbH, explains which technological challenges exist in practice, which assumptions in the design of hybrid joints often lead engineers astray and where the real economic levers lie. The discussion also addresses consequences for product architectures and validation – as well as the question of what role reversible joining may play in the future.
Mr Wäschenbach, which myth about joining metal and polymer is the most persistent – and why?
With adhesive bonding or screws we are on the safe side. These are established solutions – but often not systemically optimal ones. They increase complexity, inspection effort and risk. Nevertheless, they are often accepted because they appear to be “without alternative” or are organisationally available. The correct guiding principle is: the joint is not a detail – it is the core constructive element. Anyone who does not understand this, but somehow “solves” joining, will pay for it later in costs and may even prevent innovation.
Which challenges must metal-polymer hybrid joints face in practice?
- Different reactions to environmental influences: metals and polymers age, expand and react to temperature changes in completely different ways – this creates stresses that can weaken the joint over the long term.
- Ensuring long-term media tightness: hybrid joints must withstand diffusion, swelling and media attack for years. Water, coolants or oils change polymer mechanics and interfacial conditions – tightness is therefore not a snapshot but a long-term property.
- Material separation at end of life: with increasing regulatory requirements, disassemblability becomes a design parameter. Hybrid components must be separable without material destruction or high energy input – otherwise recycling becomes technically and economically inefficient.
Why is joining increasingly becoming a strategic topic in product development?
Because the framework conditions are changing radically. Joining technology is not a minor cost item. Depending on the product architecture, significant shares of manufacturing costs are attributable to joining processes – not only directly through cycle time and equipment, but indirectly through pre-treatment, quality assurance, rework and OEE losses.
In complex assemblies these can reach 30 % of production costs. Lightweight construction reduces structural safety margins. CO2 targets enforce material and process efficiency across the entire value chain. Regulation demands traceability and recyclability. If the joining technology cannot support this, it blocks innovation. A prominent example: Tesla had to recall around 46,000 Cybertrucks because bonded trim elements could detach. That was not a material problem – it was a joining problem. Today, joining determines scalability and competitiveness.
Hyjoin in one sentence: what is it?
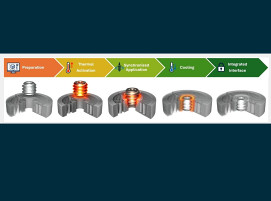
Hyjoin is a direct, induction-based joining process for metals and thermoplastics in which structured metal surfaces are used to anchor the molten thermoplastic by form fit and to produce within a few seconds a high-strength and media-tight joint without adhesives or mechanical fasteners – clean, automatable and process-reliable in series production.
In concrete terms, how does your working principle differ from adhesive bonding and mechanical joining?
We create a mechanical anchoring of the thermoplastic in a functionally structured metal surface. We do not use chemical bonding, i.e. adhesion, but primarily a form-fit and thus cohesion. As a result, the process requires no additional parts or process aids. However, the decisive difference lies not only in the working principle but in the implementation. We develop application, design-to-cost, prototyping, validation and customised industrialisation as a continuous process – and thereby assume responsibility for series capability. The greatest challenge in hybrid joining is not the first good joint – but the millionth identical one. That is precisely where industrialisation competence becomes decisive.
Which design decisions should engineering teams reconsider when using your process?
Think of joining zones as functional surfaces: Structured contact areas enable defined load transfer across a surface instead of point introduction. This allows components to be designed more compactly and additional fastening elements to be avoided. Actively control tolerances: Through locally defined energy input and controlled joining pressure, component tolerances can be compensated within a stable process window instead of having to oversize them in the design. Rethink material pairings: Material pairings previously considered critical due to lack of adhesion or thermal differences become technically manageable through form-fit anchoring – even for structurally loaded applications. The result: product architectures that were previously rejected for joining reasons become feasible. Products can be rethought.
In industrialisation, what is the greatest cost driver in hybrid joining – and how can it be avoided?
The greatest cost driver is process variability – not the nominal cycle time. The key factors are variability in pre-treatment, scrap and inspection effort, OEE losses caused by unstable process windows, and cycle time. In bonded hybrid joints, even small fluctuations in dispensing quantity or curing conditions lead to inhomogeneous interfaces – often not immediately visible, but safety-relevant. The result is increased inspection effort or hidden loss of quality. Our approach reduces process steps and eliminates consumable-dependent influencing factors. As a result, the process window is physically narrower and monitored through integrated monitoring. For us, industrialisation does not mean optimising a single project – but ensuring reproducible quality throughout the entire series production life.
When will reversible joining become a must, and when will it remain a special case?
With the new EU Ecodesign Regulation (ESPR) and “Right to Repair” initiatives, mandatory repairability and disassemblability are increasingly moving into the regulatory focus. In e-mobility and battery systems, disassembly capability becomes essential for second-life strategies and recycling. In electronics and consumer goods, requirements for repairability and material separation are becoming increasingly stringent due to regulatory measures. The technical challenge is clear: high strength and tightness during operation – combined with controlled separability at the end of life. Reversible joining will not become mandatory everywhere. However, in regulated markets it is shifting from a competitive advantage to a prerequisite. Anyone serious about hybrid design must treat joining as a strategic core technology. Anything else is merely optimisation at the margins.
Thank you for the interview.
Jakob Wäschenbach
Managing Director of Hyjoin GmbH
hy-team@hy-join.com
Schlagworte
AutomationCircular EconomyE-MobilityEnergyEngineeringInterviewJoiningJoining TechnologyJointsLightweight ConstructionPolymerPolymersQuality AssuranceSustainabilityThermoplasticThermoplastics